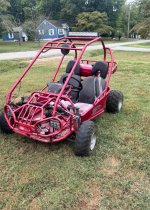
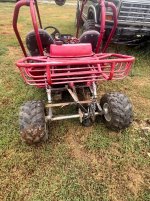
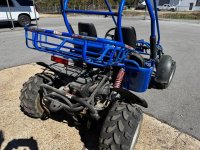
southernyankee98 — Denny and panchothedog have the right idea: you don't necessarily need a full shop of your own, but the replacement pieces need to be cut square and to length before they go to a welder, or before you weld them yourself.
A hacksaw will get you there, but it is easy to get a crooked end on thin-wall tube, and a set of matching cuts takes patience. A bandsaw — even a portable one — is kinder and faster for this. Use a fine bimetal blade, about 14 tpi or a 10/14 variable pitch, so you keep at least two or three teeth in the wall. Don't force the first cuts; a light feed for a few inches lets the honed edge wear in instead of stripping teeth. Support the tube so it can't twist or drop as the cut finishes, and keep the blade square to the work. A little wax or a drop of cutting oil helps on mild steel. Deburr the inside and outside before fit-up so the welder isn't fighting gaps.
If you want more on tooth pitch, break-in and cutting tube, there is a free book,
Metal-Cutting Band Saw Blades: Selection, Break-In, Service Life and Failure Analysis. Full disclosure, it's put out by Stankotorg, the saw shop I work for (
https://stankotorg.ru/).